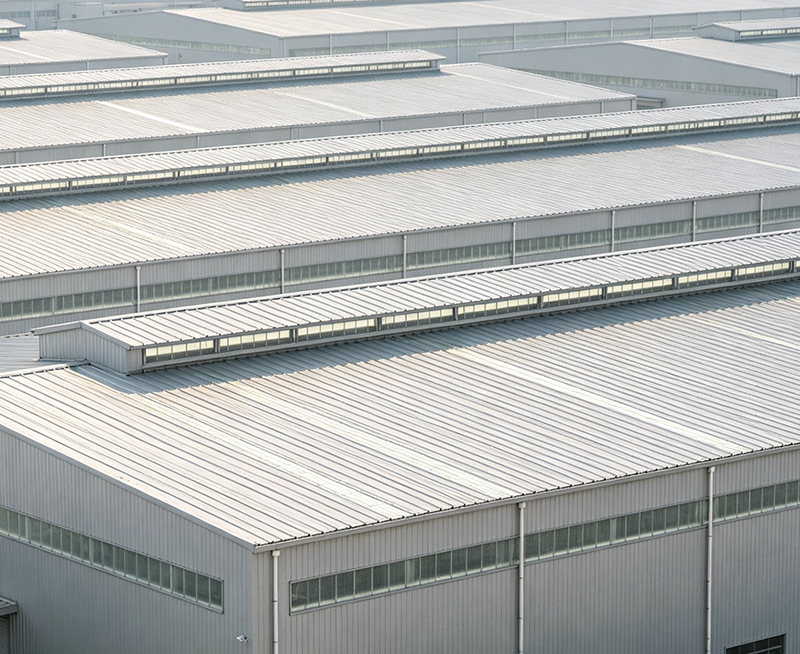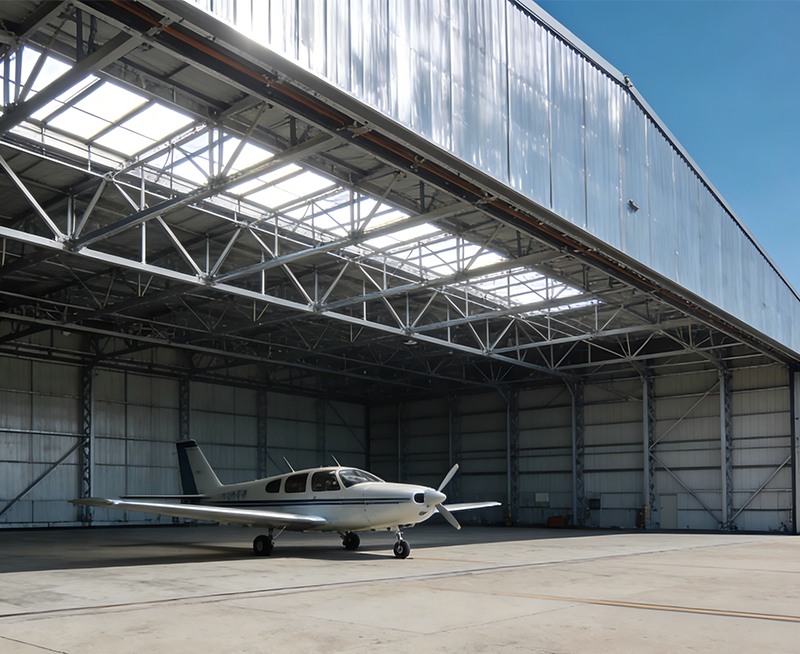


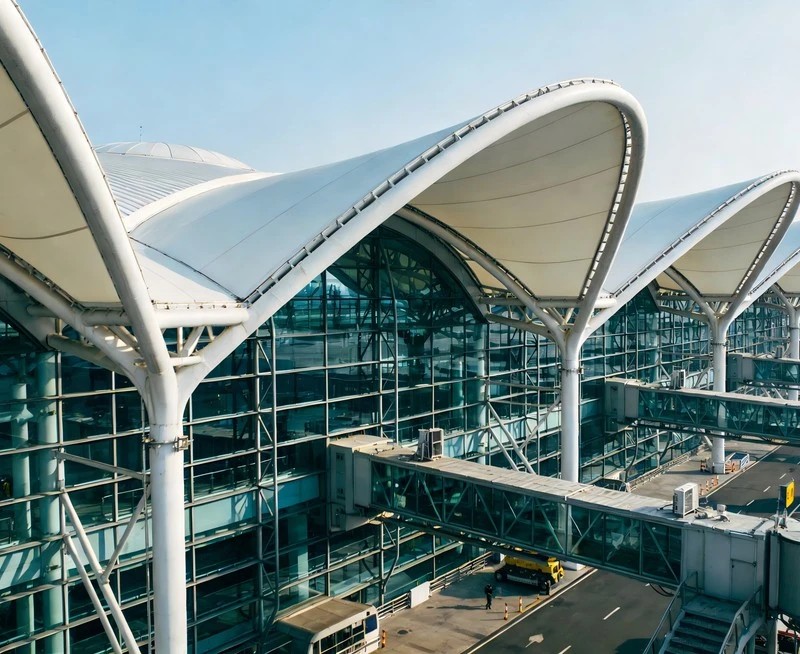
Large span steel structure connection design and fabrication control the safety, strength, and installation speed of buildings with wide column-free spaces. These buildings often include airports, sports halls, factories, warehouses, exhibition centers, and aircraft hangars.
A reliable structural steel connection transfers loads between beams, columns, trusses, arches, and foundations without creating weak points.
The design must consider steel connection detailing, load transfer, and structural stability from the first drawing to final installation.
Large roofs also face wind uplift, snow load, thermal movement, vibration, and repeated service loads.
Accurate fabrication depends on a controlled steel fabrication process, qualified welders, and dimensional inspection.
This article explains how a Large Span Steel Structures Manufacturer develops, tests, fabricates, and installs safe connection systems for long-span buildings.
Large span steel structure connections should be designed from the complete load path, checked against the selected structural standard, and fabricated with controlled welding, cutting, drilling, coating, and dimensional inspection. The best results come from early coordination between the structural engineer, steel detailer, manufacturer, and installation team. Jin'an Group can support this process through shop drawings, connection engineering, steel fabrication, quality control, and site assembly planning.
Every connection must transfer forces safely from the roof system to the main frame and then to the foundation. The engineer normally checks:
For a long-span roof, the connection is not an isolated detail. A small change in bolt location or plate thickness can affect the stiffness of the entire roof system.
The main connection types include bolted connections, welded connections, and hybrid connections. The choice depends on the force, access, transport size, installation method, and inspection requirements.
| Connection type | Main use | Advantages | Important control point |
|---|---|---|---|
| High-strength bolted connection | Beam splices, truss joints, column splices | Fast site installation and easy replacement | Correct bolt grade, tightening method, hole size, and surface condition |
| Shop-welded connection | End plates, stiffeners, box sections, node assemblies | High accuracy under factory conditions | Welding procedure, heat control, weld size, and nondestructive testing |
| Hybrid bolted and welded connection | Heavy truss nodes and transportable roof modules | Combines factory accuracy with simple site assembly | Clear division between shop work and field work |
| Pin or bearing connection | Arches, space frames, and movable support points | Allows controlled rotation or movement | Pin diameter, bearing stress, locking system, and maintenance access |
A long roof can expand and contract over its service life. The design may use fixed supports, sliding supports, expansion joints, or bearing assemblies. The expected movement should be calculated before the connection is fabricated.
For example, a steel member with a length of 100 meters and a temperature change of 40 degrees Celsius can change length by about 48 millimeters when a thermal expansion coefficient of 12 x 10-6 per degree Celsius is used. The support detail must allow this movement without damaging bolts, welds, roof panels, or foundations.
The design team should confirm the governing standard, load combinations, steel grade, fire rating, corrosion category, and inspection class before connection detailing begins. Common standards include:
One project should not mix design rules without technical approval. The engineer must define which standard controls bolt design, weld design, stability, fatigue, and acceptance criteria.
High-strength bolts are checked for tension, shear, bearing, slip, and combined actions. The design should also consider edge distance, pitch, bolt access, hole quality, and installation clearance.
Welded connections are checked for effective weld length, throat thickness, weld metal strength, base metal strength, heat-affected zones, and deformation. A weld that meets the strength calculation may still cause problems if it is difficult to inspect or paint.
Large span connections must resist more than simple member forces. Engineers should review:
Connection stiffness also affects roof deflection. A flexible joint can increase movement and change the distribution of force between nearby members.
The following workflow helps reduce design changes and fabrication delays.
Project brief and design criteria
↓
Structural analysis and load combinations
↓
Connection force report
↓
Connection type selection
↓
3D modeling and clash review
↓
Bolt and weld calculations
↓
Shop drawing preparation
↓
Engineer review and approval
↓
Material purchasing and fabrication
A connection force report should identify the maximum design forces for each important joint. It should include axial force, shear force, bending moment, torsion, load combination, and design direction.
This report helps the manufacturer understand the purpose of each plate, stiffener, bolt group, and weld. It also reduces the risk of fabricating a strong-looking connection that does not match the analysis model.
A 3D steel detailing model can identify clashes before cutting starts. The review should cover:
For complex nodes, the design team can prepare a full-size digital assembly and a physical trial assembly. A trial assembly can confirm hole alignment before the parts reach the construction site.
Steel plates and sections should be identified when they arrive at the factory. The manufacturer should compare the material grade, thickness, heat number, quantity, and mill certificate with the approved material list.
Typical control records include material receiving reports, traceability tags, cutting plans, welding logs, inspection reports, and coating records.
Computer-controlled plasma or flame cutting can produce accurate plates when the machine is correctly calibrated. A typical fabrication plan may use:
Drilled holes should be clean and free from excessive burrs. Flame-cut holes should only be used when they meet the approved project requirements. Enlarging holes at the site without engineering approval can reduce connection capacity.
Welding should follow an approved welding procedure specification. The procedure should define the welding process, filler metal, preheat temperature, interpass temperature, position, sequence, and inspection level.
Common inspection methods include:
The required test percentage depends on the design code, weld category, risk level, and project specification. Critical tension welds may require a higher inspection rate than secondary attachments.
Before final welding, fabricators should check root gaps, plate alignment, member orientation, bolt holes, stiffener location, and overall dimensions.
For a complex truss node, the factory can assemble connected parts in a controlled area. The inspection team can record diagonal measurements, flange levels, hole alignment, and contact surfaces. This step can prevent expensive site correction.
Quality control should be divided into receiving inspection, in-process inspection, and final inspection.
| Stage | Inspection item | Example record or measurement |
|---|---|---|
| Material receiving | Grade, thickness, heat number, surface condition | Mill certificate and traceability tag |
| Cutting | Plate shape, edge condition, length, and width | Inspection report against approved shop drawing |
| Drilling | Hole position, diameter, spacing, and burr condition | Calibrated ruler, gauge, and coordinate check |
| Fit-up | Root gap, alignment, squareness, and orientation | Fit-up inspection before welding |
| Welding | Weld size, visual quality, procedure, and welder qualification | Welding log and visual inspection report |
| Nondestructive testing | Surface or internal weld defects | MT, UT, or RT report as specified |
| Coating | Surface preparation and dry film thickness | Surface profile and coating thickness readings |
| Final inspection | Dimensions, marking, packing, and documents | Final release checklist |
Large connection assemblies should be measured at several stages. Typical checks include overall length, width, height, diagonal difference, flange level, bolt-hole position, and connection angle.
The allowable tolerance should follow the approved drawing and applicable execution standard. A general tolerance should not replace a project-specific tolerance for critical nodes.
Steel connections may use paint systems, galvanizing, or a combination of protection methods. The specification should define surface preparation, primer type, intermediate coat, topcoat, total dry film thickness, repair method, and exposure category.
Bolted faying surfaces need special attention. Paint can change slip resistance if the connection is designed as a slip-critical joint. The coating system must match the bolt design and project specification.
| Factor | Bolted connection | Welded connection | Hybrid connection |
|---|---|---|---|
| Factory work | Moderate | High | High for node assembly |
| Site work | Fast when access is good | Slower and more weather-sensitive | Moderate |
| Inspection | Bolt and hole inspection | Visual and nondestructive weld testing | Both bolt and weld inspection |
| Transport | Easy to split into smaller modules | Large welded nodes may be heavy | Suitable for controlled modular delivery |
| Future modification | Usually easier | Requires cutting and rewelding | Depends on the detail |
| Main risk | Incorrect tightening or poor hole alignment | Welding defects and distortion | Poor coordination between shop and site work |
Jin'an Group can organize large span steel structure projects through a coordinated process that links design review, steel detailing, procurement, fabrication, inspection, packing, and installation support.
This integrated method reduces information gaps between the design office and the steel workshop. It also helps the project team confirm transport limits, lifting points, splice locations, and site bolt access before production.
For each project, the production plan can divide the work into material receiving, cutting, assembly, welding, trial fitting, surface treatment, final inspection, and delivery. The inspection plan should identify hold points before major work continues.
Useful project controls include:
Connection research and development should focus on reducing steel weight, improving erection speed, increasing repeatability, and making inspection easier. Practical development topics include modular truss nodes, bolted splice systems, adjustable support details, lifting devices, and connection designs that reduce field welding.
A manufacturer can measure development results through fewer site modifications, lower assembly time per joint, reduced welding length, improved dimensional accuracy, and a lower number of nonconformance reports. These measurements provide a clearer result than using general claims such as high quality or advanced technology.
Cause: Incorrect survey data, accumulated fabrication tolerance, or drawing revision errors.
Solution: Use one controlled 3D model, verify the reference grid, inspect hole locations before shipping, and conduct a trial assembly for complex joints.
Cause: Uneven heat input, poor welding sequence, large weld volume, or insufficient temporary restraint.
Solution: Use a qualified welding procedure, balanced weld sequences, controlled preheat, temporary fixtures, and dimensional checks between welding stages.
Cause: Insufficient wrench clearance, poor lifting access, hidden bolts, or an assembly sequence that was not reviewed.
Solution: Review the erection sequence in the 3D model. Check crane access, temporary stability, bolt installation space, and safe worker access.
Cause: Unapproved hole enlargement, field cutting, or welding without a qualified procedure.
Solution: Use a formal technical query process. Require engineer approval before any change to a primary connection.
Cause: Poor surface preparation, damaged coating, water retention, or an unsuitable coating system.
Solution: Seal water traps, repair damaged areas, record coating thickness, and match the protection system to the exposure environment.
When selecting a large span steel structures manufacturer, the buyer should ask for clear answers to the following questions:
Large span steel structure connection design and fabrication require more than strong materials. The project needs a complete load path, suitable bolt and weld details, controlled movement, accurate shop drawings, qualified fabrication, and documented inspection. Standards such as AISC 360, EN 1993-1-8, EN 1090-2, AWS D1.1, and ISO 3834 help define the design and quality requirements. With coordinated engineering, measurable production controls, and careful site planning, Jin'an Group can help deliver safe and efficient large span steel structures for complex building projects.
Produits associés